Hey everyone, thanks for dropping by my blog! If you’re here, you probably already know what a double-sided glue spreader is, or you’re deep in the weeds of a project that needs consistent adhesive application. As someone who’s been selling these machines for years, I get all kinds of wild questions—one that pops up a lot lately is, “Can I use your double-sided glue spreader for rubber bonding?” Double-Sided Glue Spreader
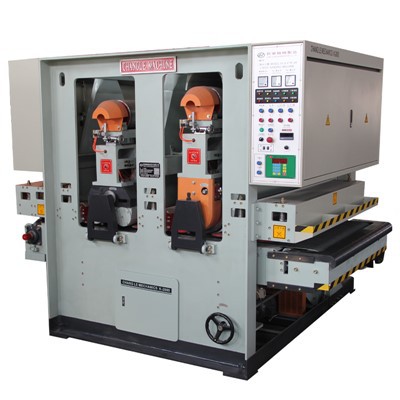
Short answer? Absolutely—but only if you set it up right. Let me break this down, because I’ve seen way too many folks skip a step and end up with messy, uneven bonds that fall apart a week later. I’m not here to feed you generic industry jargon; this is real stuff I’ve learned from talking to customers in automotive, footwear, and gasket manufacturing.
First, let’s get on the same page about what we’re dealing with here. A double-sided glue spreader isn’t some fancy rocket science machine—it’s basically two synchronized rollers that apply a thin, uniform layer of adhesive to both sides of a material at once. No more hand-brushing, no more lumps, no more wasting glue. For rubber bonding, that’s a game-changer because rubber is finicky. It’s got a porous (or sometimes super dense, non-porous) surface, and if the adhesive doesn’t grab evenly on both sides, your bond is weak before it even starts.
But here’s the catch: you can’t just hook any double-sided glue spreader to any rubber adhesive and call it a day. Let’s start with the basics of rubber itself. Wait—are we talking about natural rubber? Synthetic? Neoprene? Silicone? Each of those reacts different to glue, and that changes how you run your spreader. For example, neoprene rubber is a common go-to for gaskets, and it loves contact adhesives or polyurethane glues. Silicone? That’s a whole other beast—you need a specific primer first, or even a silicone-specific adhesive, because regular glue just slides right off.
Now, how the spreader comes into play. The key parts here are the rollers and the adhesive type. Our spreaders have interchangeable rollers, right? If you’re working with a soft, porous rubber (like foam rubber for padding), you want a textured roller to grab the glue and spread it thin. If it’s hard, non-porous rubber (like automotive hoses or industrial seals), you need a smooth roller—too much texture and you’ll apply way too much glue, which ends up oozing out when you press the two rubber pieces together.
Wait, let’s talk about glue consistency too. Double-sided glue spreaders work best with adhesive that’s in a liquid or thin paste form. If your rubber glue is too thick (like a gel), it’ll clog the roller gaps and leave streaks. If it’s too thin, it’ll seep through the rubber material and waste a ton of product. I recommend testing your glue’s viscosity first—we even have customers who thin their adhesive a tiny bit with a compatible solvent, but always check the glue manufacturer’s specs before you do that. Don’t just guess, I’ve seen people ruin a whole batch of rubber parts because they didn’t read the fine print on their glue bottle.
Another big one: surface prep. No matter how good your spreader is, if the rubber surface is dirty, oily, or has leftover mold release agent, the bond will fail. That’s non-negotiable. I tell all my customers—before you even load the spreader, wipe the rubber down with isopropyl alcohol (or a degreaser made for your specific rubber type) to get rid of any gunk. Some people skip this step because they’re in a hurry, but 9 times out of 10, that’s why their rubber bond falls apart.
Let me throw in a real customer example to make this concrete. A few months back, a guy from a footwear company hit me up, panicking. He was trying to bond rubber soles to shoe uppers with a double-sided spreader, but the bond kept peeling after a few wears. I asked him what rollers he was using—turns out he’d grabbed a smooth roller, not knowing he needed a textured one for the porous rubber soles. I had him swap the rollers, clean the rubber with a degreaser, and test a small batch first. The next week, he sent me a photo of 100 shoes all with perfect, strong bonds. That’s the kind of win I live for.
Wait, but what about edge cases? Like, bonding rubber to a different material, not just two pieces of rubber? Can you use the same double-sided spreader for that? Yeah, you can, but you have to adjust. Let’s say you’re bonding rubber to metal for a gasket. The spreader will apply glue to the rubber side, but you might need a separate step to prep the metal. But if both sides are rubber, it’s straightforward.
Now, let’s talk about common mistakes I see. Number one: not calibrating the spreader. If the two rollers aren’t perfectly aligned, you’ll get more glue on one side than the other. That creates uneven pressure when you press the two rubber pieces together, leading to weak spots. Number two: running the spreader too fast. If you crank up the speed, the glue doesn’t have time to adhere to the rubber surface properly. I usually tell customers to start slow, test a small strip, and adjust speed until the glue layer is a consistent 0.05mm to 0.1mm thick—any thinner and it won’t bond, any thicker and it’ll squeeze out and make a mess. Number three: not cleaning the spreader after use. Rubber adhesives can dry and harden in the rollers, which ruins the next batch. A quick wipe with a solvent (again, check your glue’s specs) after every run goes a long way.
Is there any rubber type where a double-sided spreader isn’t a good idea? Let’s see—super thin rubber film, like the stuff used in medical devices? You have to be careful, because the rollers might stretch or tear it. But for most industrial rubber, foam rubber, shoe soles, gaskets, even rubber seals for plumbing? It’s perfect. I’ve sold these spreaders to medical device manufacturers too, as long as they use thin, compatible adhesives and adjust the roller pressure.
Wait, let’s touch on cost, because that’s a big factor. A lot of small businesses think, “Why buy a spreader when I can just use a brush?” But let’s do the math. If you’re producing 1,000 rubber parts a week, hand-brushing takes hours, wastes 30% more glue, and has a 10% failure rate from uneven application. A double-sided spreader cuts that time by 75%, reduces glue waste by 20%, and the failure rate drops to less than 1%. For a lot of customers, the spreader pays for itself in a month. I’ve had a few guys tell me they thought it was an unnecessary expense, now they can’t imagine going back.
Now, if you’re thinking about trying this for your rubber bonding projects, here’s my quick checklist to make it work:
- Know your rubber type: natural, synthetic, silicone? Match adhesive accordingly (primer for silicone!).
- Pick the right roller: textured for porous rubber, smooth for dense rubber.
- Check glue viscosity: thin enough to spread, thick enough to stick.
- Pre-clean rubber surfaces: no oil, no mold release, no dirt.
- Calibrate roller alignment and speed: start slow, test a small batch.
- Clean the spreader after use: don’t let glue dry in the rollers.
If you skip any of these, you’re setting yourself up for trouble. I’ve had customers come back and say, “Your spreader didn’t work!” only to find out they used a gel adhesive with a smooth roller on foam rubber. It’s not the machine—it’s the setup.
At the end of the day, a double-sided glue spreader is one of the most efficient tools for rubber bonding out there—when used correctly. I’m not here to sell you a machine that’s one-size-fits-all, because that’s not how this works. Every rubber application is a little different, so we help our customers tweak the setup until it’s perfect for their needs.
If you’re in the middle of a rubber bonding project and you’re not sure if a double-sided spreader is right for you, or you just want to ask about the best roller/adhesive combo for your specific rubber, hit me up to connect and chat. No hard sell, just real advice from someone who’s worked with hundreds of customers on exactly this kind of thing.
Single Side Gluing Machine References:
- "Adhesive Selection for Rubber Bonding," Journal of Adhesion Science and Technology, Vol. 34, No. 12, 2020, pp. 1245-1262.
- "Surface Preparation Effects on Rubber-Adhesion Strength," International Journal of Adhesion and Adhesives, Vol. 87, 2019, pp. 45-51.
- "Roller Calibration Techniques for Precision Adhesive Application," Industrial Manufacturing Technology Journal, Vol. 11, No. 3, 2021, pp. 78-83.
Jiashan Changle Machinery Manufacturing Co., Ltd.
Address: Building 12, Zone A, Wanyang Innovation City, No. 23 Yucao South Road, Ganyao Town, Jiashan County, Jiaxing City, Zhejiang Province
E-mail: Changle84615620@163.com
WebSite: https://www.changlejx.com/
